Skip to content
- Key Takeaways
- Why Certifications Matter in Commercial Blender Procurement
- CE Certification for Commercial Blenders (EU Market)
- UL Certification for the U.S. Market
- NSF Certification & Food Contact Compliance
- FDA, LFGB & Food-Grade Material Regulations
- CB Scheme & Multi-Country Certification Strategy
- Middle East & Emerging Market Requirements
- Certification Checklist for Importers
- OEM Compliance Pipeline: How Professional Manufacturers Handle Certification
- How to Avoid Certification Fraud in the Blender Industry
- Final Thoughts: Choosing a Certification-Ready Commercial Blender Supplier
- Frequently Asked Questions
Key Takeaways
- Many distributors who are familiar with key certifications like CE, UL, NSF, FDA and LFGB can easily weed out unsafe or non-compliant commercial blenders before they reach a kitchen or retail channel. This expertise directly decreases legal exposure and safeguards end users from electrical, fire, and hygiene hazards.
- In the European Union, credible CE marking rests on a complete technical file that covers risk assessment, test reports, and correct labeling under the Low Voltage, EMC, and relevant Machinery Directives. Importers and distributors should always request this documentation and verify that it actually matches the blender model being supplied.
- In the U.S., UL listing is a useful standard for electrical and fire safety with commercial foodservice equipment. UL Recognized components aren’t a replacement for a listed appliance. Stakeholders who differentiate between these marks can avoid equipment that looks compliant but doesn’t pass local inspection or insurance requirements.
- Food contact safety involves more than one logo, so decision makers should look for NSF certification for hygiene and sanitary design, as well as FDA or EU LFGB compliance and clear statements on BPA-free plastics and food-grade stainless steel. This mix approach mitigates compliance risk that blender parts contacting food are not only chemically safe but simple to maintain in high-volume kitchens.
- Global distributors can simplify multi-country market entry by leveraging the CB Scheme and mapping out a certification journey that transforms a single core test program into multiple approvals, including the GCC and SASO as applicable. This organized approach saves duplicated testing expenses and reduces time to market across countries.
- To prevent certification fraud, procurement teams need to proactively cross-check test report numbers, issuing lab accreditation, validity dates, model consistency and factory audit records, preferring OEM partners that run an open compliance pipeline. Putting this checklist to work for each new blender supplier gives you a repeatable, low-risk process for long-term sourcing.
Why Certifications Matter in Commercial Blender Procurement
Certifications provide purchasers explicit evidence that a commercial blender is safe, can be legally used in their jurisdiction, and is designed for intense daily efforts in a bustling kitchen or bar. They transform ambiguous assertions into marks that a neutral party has examined and verified.
UL and ETL marks demonstrate the unit survived rigorous electrical and fire safety testing, reducing the risk of shocks, burns or motor defects. CE Marking in the European Economic Area is not optional. It demonstrates the blender complies with EU safety and health requirements, so purchasers don’t risk legal complications and import restrictions.
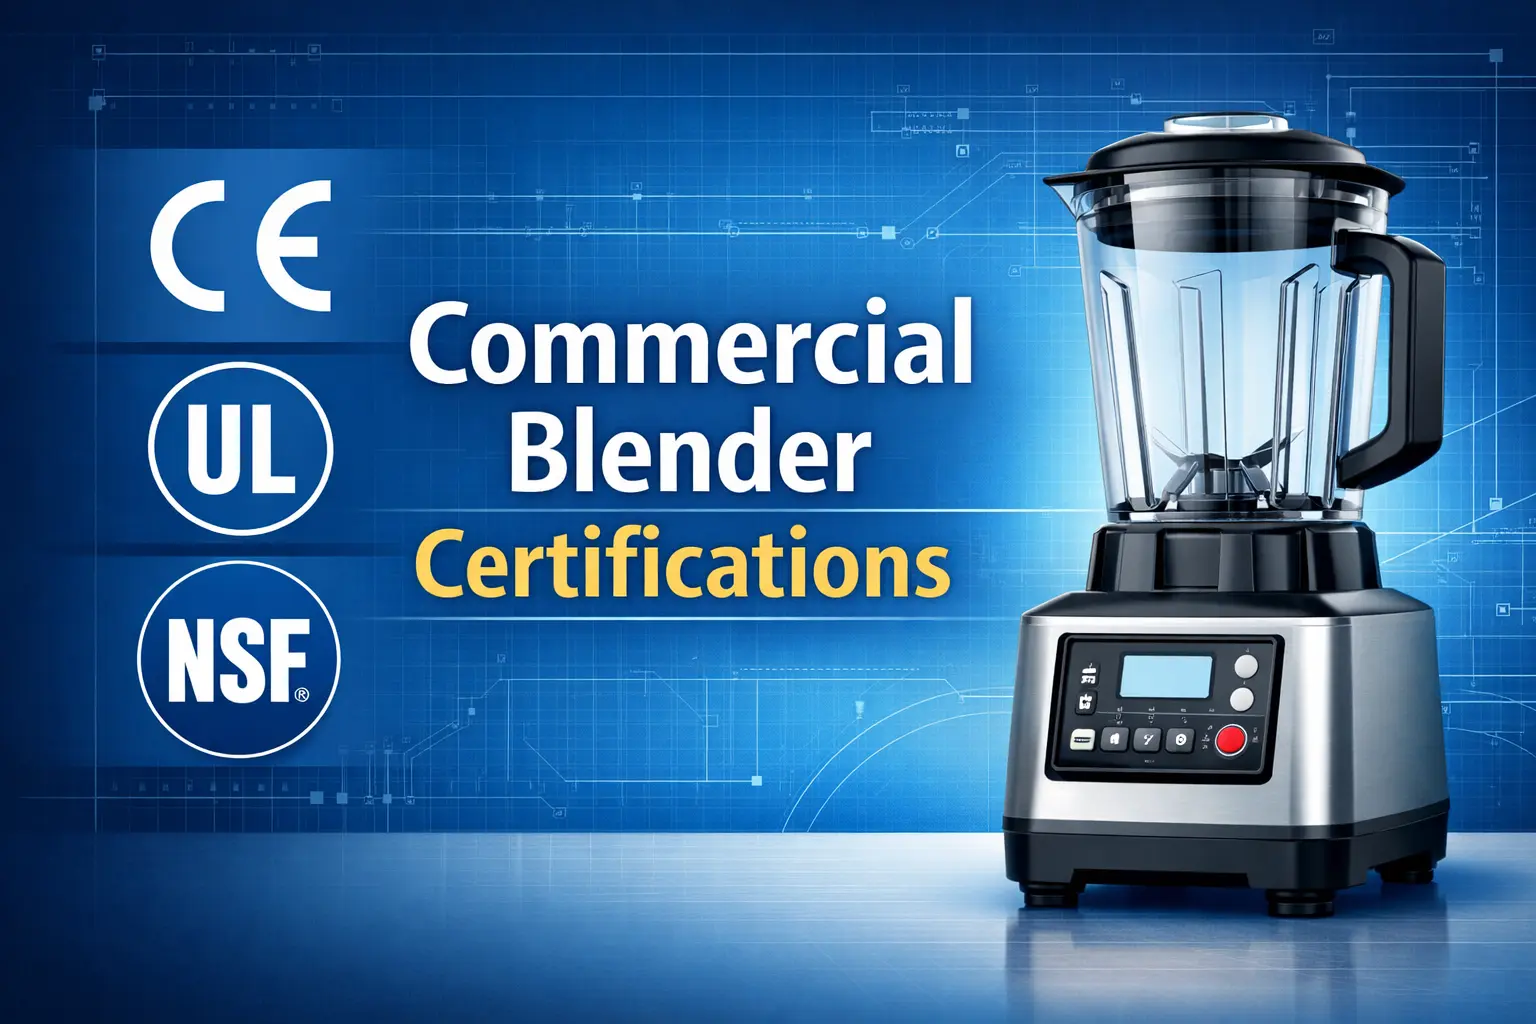
Commercial blender certifications are not just regulatory formalities. They directly determine whether a high-power blender can be legally imported, installed, insured, and used in commercial kitchens across different markets. Understanding commercial blender certifications allows distributors to minimize compliance risk and protect long-term business operations.
This guide is written from an OEM and compliance engineering perspective, focusing on high-power commercial blender platforms used in professional kitchens, hospitality chains, and distribution networks.
CE Certification for Commercial Blenders (EU Market)
CE certification is one of the most critical commercial blender certifications required for entry into the European market.
CE marking on a commercial blender signifies compliance with fundamental EU standards relating to safety, health, electromagnetic emissions, and energy consumption. Its absence bars the product from legal sale in the EU or EEA.
According to the European Commission guidance on the Low Voltage Directive, manufacturers are responsible for compiling and maintaining technical documentation for at least 10 years after the product is placed on the market.
What CE Actually Covers
For most CE commercial blender models, testing is performed according to EN 60335-1 (General requirements for household and similar electrical appliances) and EN 60335-2-14 (Particular requirements for kitchen machines). EMC compliance typically references EN 55014-1, EN 55014-2, and EN 61000 series standards. Additionally, RoHS Directive 2011/65/EU and REACH Regulation (EC) No 1907/2006 may apply to material restrictions.
The Electromagnetic Compatibility (EMC) Directive guarantees that the blender will not interfere with other devices and will continue to function in a “noisy” electrical environment, such as a bustling café. This is what conducted and radiated emissions testing, immunity to electrostatic discharge, and surge tests are all about, typically performed in an accredited lab using harmonized EN standards.
EU Machinery Regulation (EU) 2023/1230 can apply when a blender has complex or automated functions, such as integrated dosing, interlocked lids, or automatic cycles that move blades at high speed. It centers on mechanical hazards, guards around blades, safe opening of jugs, and emergency stop behavior and clear safety instructions. Hand-powered blenders remain outside this scope, so they are not typically affected by that same CE framework.
Technical File & Declaration of Conformity
Behind every CE mark has to be a technical file which proves how the blender complies with the regulations. This file is not a marketing brochure; it’s a hard structured evidence pack that they can request at any time during surveillance of the market.
Risk assessment sits at the core of that file. Engineers list every “reasonably foreseeable” hazard: electric shock from damaged cords, cuts from exposed blades, burns from hot soup, micro‑switch failure on the lid, instability on wet counters. For each item, they describe the design measure used to lower the risk. For example, double insulation, lid interlocks, non‑slip feet, overload protection, or clear warning labels.
Test reports support this risk reasoning. Manufacturers or their labs execute type tests to EN 60335-1 and EN 60335-2-14 as well as relevant EMC standards. The reports capture test setups, measurement data, and pass/fail decisions for dielectric strength, leakage current, endurance, EMC emissions, immunity, and energy performance under Regulation (EU) 2019/2020 establishing minimum energy efficiency index levels and the A–G energy label scheme. For large hotel or restaurant purchasers, these reports become a part of vendor qualification.
Labeling finishes the circle. The blender has to display the CE mark, manufacturer name and address, model ID, rated voltage and power, as well as any required symbols, such as the protection class and food contact symbol. EU 2019/2020 energy labels conform to the usual A to G scheme with consistent units and icons, so purchasers anywhere in the Member States can easily compare models.
Overall, the adherence to industry standards ensures that blenders not only meet safety requirements but also maintain high quality for consumers. This process ensures regulatory conformity and traceable compliance documentation.
Common Misconceptions About CE Marking
A common misconception is that CE marking is always issued by a government authority or a notified body. It doesn’t mean ‘mark it and hope’. The manufacturer still has to conduct or outsource all necessary testing, maintain the technical file and sign the DoC. A notified body only gets involved when a particular regulation requires third-party involvement for that type of product or level of risk or when the manufacturer elects to use them to generate additional trust with large customers.
Yet another common issue is fake and misleading CE marks in OEM chains. Some cheap manufacturers put a “CE-like” mark that’s not in the legal proportions or “China Export” style markings that attempt to resemble it. Brand owners that purchase such blenders and re-label them for the EU can still be considered the manufacturer in the eyes of the law, which means they bear the legal risk if the CE claim is fraudulent.
OEM design changes have a greater regulatory impact than many distributors initially assume. If a distributor requests the factory to “tune” the motor power, bypass safety switches, or replace blades to slice through thick frozen mixes, that can alter the risk profile and even violate LVD, EMC, or the Machinery Regulation. Once an end user alters the blender after sale, say by semi bypassing a lid sensor or installing non-approved jars, then the original CE mark doesn’t cover that modified product any longer, and the manufacturer generally isn’t responsible for ensuing problems.
UL Certification for the U.S. Market
Among global commercial blender certifications, UL plays a central role in U.S. market access.
UL certification is the hub of the way the U.S. Handles safety for commercial blenders and other food-service machines. It dictates what can be sold, installed, insured, and inspected in real kitchens. And UL certification is issued by Nationally Recognized Testing Laboratories (NRTLs) recognized by OSHA in the United States.

What Is UL Listing?
UL Listing means a completed product has passed a specific set of safety tests and periodic follow-up inspections. For a commercial blender, this centers on electrical safety. UL looks at insulation breakdown, leakage current, grounding, and strain relief on power cords. They verify clearances between live parts, overcurrent protection, and the unit’s behavior under abnormal conditions, such as blocked vents or low supply voltage. Tests include durability of switches and connectors with heavy, repeated use such as that which is common in cafés or quick-service chains.
Fire risk evaluation adds another layer. UL studies how hot components, such as motors and control boards, behave during long duty cycles. They check enclosure materials for flammability, wiring routing, and whether internal faults could start a fire at the counter or inside cabinetry. More than 40,000 U.S. Jurisdictions recognize the UL mark, so these test outcomes directly influence local approvals, from small-town inspectors to large city fire departments.
Difference Between UL Listed and UL Recognized
UL Listed is for the final product, like a high-volume commercial blender you can plug into a 120 V or 240 V outlet at a café. The unit as a whole is evaluated as a system, including housing, controls, and power connection, and is then labeled for particular installation and usage circumstances.
UL Recognized is not the same. It encompasses any parts, such as a motor, power supply, or relay found within the blender. These components comply with some safety standards but are not independent products. The blender maker needs to engineer and test the entire machine so these certified parts still satisfy the final UL standard.
For distributors, it’s a UL Listed blender that counts. It means UL has reviewed the entire appliance, not just the components within, and that the item can be tested specifically to standards and insurance needs.
Why UL Matters for Commercial Kitchen Equipment
In the United States, commercial blenders are commonly evaluated under UL 982 (Motor-Operated Household Food Preparing Machines) or related food-service appliance standards depending on configuration and power rating.
Understanding commercial blender certifications is essential for distributors seeking long-term regulatory stability.
NSF Certification & Food Contact Compliance
How NSF certification and food contact rules influence the real-world safety of commercial blenders.
What NSF Certification Covers

NSF certification examines hygiene standards in a practical manner. It tests whether a blender can be sanitized quickly and thoroughly between batches, if food soil rinses off, and if no obscured crevices entrap smoothies, sauces, or dairy. Inspectors examine written cleaning procedures, test how parts detach and reattach, and verify that the unit withstands repeated wash cycles without parts warping and seals breaking.
Sanitary design is at the heart of the NSF checklist. They seek out smooth, sealed seams on the jar, base, and control panel. They ensure that screws, gaskets, and couplings do not sit in “splash zones” where food can accumulate. Vent slots, fans, and motor housings require open airflow and yet must block liquid drips into the electronics, which is common in bars and central kitchens.
Material safety represents the final pillar of hygienic compliance. NSF examines the very plastics, rubbers, and metals the blender manufacturer employs in any location that can contact food, ice, or steam. They test migration limits to ensure that monomers, plasticizers, or heavy metals are far below risk levels even in hot soups or acidic blends.
NSF certification for commercial blenders is typically assessed under NSF/ANSI 8 (Commercial Powered Food Preparation Equipment), which evaluates cleanability, material safety, and sanitary design.
NSF vs FDA Food Contact Compliance
NSF and FDA do very different jobs. FDA defines the baseline criteria for food-contact materials. NSF evaluates entire blender designs during actual use.
FDA, LFGB & Food-Grade Material Regulations

Commercial blender purchasers typically inquire if jars, lids, and gaskets satisfy FDA or LFGB rules, as those components remain in prolonged, direct contact with food.
U.S. FDA food contact compliance is governed under 21 CFR Parts 170–199, particularly 21 CFR 177 for polymeric materials. EU food-contact compliance is primarily regulated under Regulation (EC) No 1935/2004 and Regulation (EU) No 10/2011 for plastic materials.
U.S. FDA food contact regulations
Importers evaluate plastics and silicone components that come into contact with food to verify compliance with applicable migration limits and toxicological standards. In the case of silicone lids or gaskets, FDA laws verify that no hazardous levels of additives transfer into smoothies, soups, or crushed ice. The jurisdiction is oftentimes perceived as less rigorous than German or EU laws. It still provides an explicit safety floor that cafes, juice bars, and small kitchens in North America can rely on as a baseline when they compare brands.
EU food contact framework
Distributors and compliance teams monitor the general EU food-contact framework tying together Regulation (EC) No 1935/2004, Plastic Regulation (EU) No 10/2011, and the German Food and Daily Necessities Act, primarily LFGB Articles 30 and 31. If a blender jar or silicone seal meets these, the manufacturer can mark it with the “knife and fork” symbol that designates approved food contact throughout the EU. This covers heavy metals, VOCs, PAHs, extractable chemicals, odor and taste transfer, so you don’t get that plastic smell in a smoothie. France and Germany request LFGB on silicone goods sold in their markets, which comes into play when a café chain is in both Berlin and Paris.
BPA-free requirements
Importers usually anticipate BPA-free markings on polycarbonate or alternative plastic jars as BPA has caused long-standing health concerns at low migration levels. They then cross-reference that label with FDA or EU test reports to determine if their blender maker used some alternative resins that still meet food-contact regulations and don’t degrade due to exposure to hot soups or extended blending cycles. In practice, this means selecting BPA-free jars that meet FDA and EU limits on overall migration, so the jar remains crystal clear, impact resistant, and safe for everyday use. When data exists, they verify through specific migration tests under worst-case use, such as high-fat foods at high temperature.
Stainless steel food-grade standards
Distributors often assume stainless steel jars and blades are automatically food-grade; however, verification of material grade and surface finish is essential. A discerning buyer verifies that welds, seams, and blade hubs utilize the same grade steel and smooth surface finish because rough, inferior joints can harbor food, increase bacteria proliferation, or leach nickel and chromium. For worldwide use, they seek evidence that the steel parts comply with EU food-contact legislation, Japanese Food Sanitation Act standards, and any additional LFGB metal release tests, not generic “stainless” assertions in a brochure. Over time, this helps them select blenders that maintain both sanitary and flavor consistency under intense daily load.

CB Scheme & Multi-Country Certification Strategy
The CB Scheme provides one test path for commercial blenders that require certifications in multiple markets, so they don’t begin anew for each country. It operates on IEC safety standards for motors, blades, controls and enclosure design, similar to what labs use in the EU, Asia and the Americas. A lab produces a single CB test report and certificate, and many national bodies rely on it to issue national marks more quickly, reducing duplicate testing, sample numbers and lab fees. For global distributors, this lets them strategize one core blender platform, change out only plugs or markings for each market, and keep safety files in sync as IEC rules evolve.
Middle East & Emerging Market Requirements
Commercial blender regulations in the Middle East and emerging markets are based heavily on local cuisine, electrical limitations, and rigorous safety inspections. These are things that not all international brands pick up on early.

SASO (Saudi Arabia)
In Saudi Arabia, for example, any commercial blender has to comply with SASO electrical safety regulations that are frequently connected to particular plug types, voltage, and thermal cut-off tests, in addition to explicit Arabic labeling. Ice, dates, and spice mix crushing units for juice bars or hotel buffets require powerful motors and blades, yet must still clear noise and durability tests under local test procedures. If a blender adds smart controls or Wi-Fi, SASO may pull in radio and EMC rules, which pushes brands to align hardware, firmware, and power supply design pre-shipment to skirt port delays.
GCC compliance
Throughout GCC states, they come against GCC Standardization Organization regulations that encompass common electrical safety, energy consumption, and food-contact restrictions. A blender approved in one GCC country can usually slip through the others a little quicker, but only if test reports, certificates of conformity, and manuals are aligned with recent GSO standards and language requirements. Hoteliers, juice bars, and chains employ this to select models that can pump heavy loads, such as frozen fruit or tahini bases, yet still pass standard tests on overheating, leakage current, and food contact.
Local registration issues
Outside of the GCC, every emerging market has its own registration labyrinth — from importer licenses and local lab testing to clearance for spare parts and service stations. Asia-Pacific distributors, for instance, need blenders that can withstand bubble tea pearls, frozen smoothies and street food preparation, while rapid urbanization and menu changes are forcing vendors to combine high load cycles with smaller footprints. Meanwhile, e-commerce makes blenders simpler to purchase but more difficult to monitor, so brands have to align certificates, serial tracking and customs information or face confiscation or quiet prohibitions.
Certification Checklist for Importers

Importers require a definitive checklist that they are not simply buying commercial blenders across borders on faith.
| Certification | Primary Market | Covers | Mandatory for Import? | Risk if Missing |
|---|---|---|---|---|
| CE | European Union | Electrical safety, EMC, mechanical risk | Yes | Customs rejection, legal liability |
| UL | United States | Electrical & fire safety | Strongly required in commercial kitchens | Insurance refusal, inspection failure |
| NSF | U.S. & Global Foodservice | Hygiene & sanitary design | Often required by chains | Health inspection issues |
| FDA / LFGB | U.S. / EU | Food-contact material safety | Yes (for food contact parts) | Product recalls, compliance fines |
| CB Scheme | Multi-country | IEC safety testing | Not mandatory but strategic | Duplicate testing costs |
Request valid test report (with report number)
Importers should request complete test reports rather than summary certificates. The bill of materials referenced in the test report must match the components used in production. For sales in Europe, they should tie the test report to an EU Declaration of Conformity and verify that all applicable directives like Low Voltage, EMC, and RoHS are indicated. If a report conceals test methods, limit values, or failure data, that’s a red flag.
Verify issuing lab accreditation
Compliance verification requires confirmation that the issuing laboratory holds valid accreditation for the applicable standards. This involves verifying the lab’s accreditation number on the report and cross-referencing it with bodies’ databases such as ISO/IEC 17025 accreditation agencies. If a blender is going to Europe and North America, they want to know the lab can test to EN and UL/CSA. When the lab is elsewhere, they have to see if its accreditation is recognized under mutual recognition agreements in the destination market.
Confirm product model consistency
Importers must verify that the tested model is identical to the production model being shipped. They contrast photographs, nutrition score labels, measurements, jar capacity in litres, motor wattage, and control panel configuration. Importers need to ask for tolerance drawings for critical components like jar necks, couplings, and blade hubs and verify that they coincide with what the test report states. They then inquire if the supplier utilizes go/no-go gauges on these fits and conducts straightforward statistical checks during daily mass production to ensure that the blender in the lab and the blender in the restaurant are identical.
Check validity period
Importers must verify that reports and certificates remain valid and address current standards, as safety and EMC regulations frequently evolve. Most marks have defined expiry dates or surveillance cycles, so the importer verifies both the report date and any follow-up audit records. If the supplier has made a design change, such as a new motor supplier, new control board, or jar material shift, they should verify if a retest or update letter is on file. They verify for new markets if local rules, such as energy, safety, health, or environment rules, have been added since the initial approval.
Review factory audit documentation
Regulatory due diligence requires review of factory audit documentation. A proper checklist spans legal registration, ownership, and sub-factory use, along with a walk-through of the production line, incoming checks and final inspection. Importers should request certification that lists equipment, daily capacity, and quality tools, and whether the supplier uses go/no-go gauges inline and monitors defects for trends. When they visit in person, they observe the actual assembly flow, determine how many workers are cross-trained, and find out if crucial steps such as torque, blade fit, and leak checks depend on a single ‘expert’ or on defined, repeatable work processes. In that way, they connect the certifications, the factory’s control system, and the blender their own customer will hold in hand.
Experienced OEM manufacturers integrate certification planning during the product development phase, rather than treating it as a post-production checkbox.
OEM Compliance Pipeline: How Professional Manufacturers Handle Certification

Professional OEMs develop a repeatable compliance pipeline so their commercial blenders clear food-contact, safety, and performance regulations in every target market.
Pre-certification design review
Beginning with a design review that maps every part to rules such as EU REACH, EU 1935/2004, FDA food-contact and Japan’s Food Sanitation Act. They pick food-safe materials, often Tritan copolyester for jars and stainless steel for blades and housings, and verify hygienic design principles like smooth welds, no dead zones, and gaskets that are easy to remove and clean. At this point they plan for 3-A, NSF 538 MOAH-Free, and ISO 21469 needs, so seals, lubricants, and plastics do not leak unsafe chemicals into food.
EMC pre-scan testing
Before taking units to an accredited lab, they run EMC pre-scans in-house or with a partner test site. They test emissions from the motor drive, power supply, and control board, as well as immunity to static discharge and power line noise. Typically, the engineers then adjust filters, grounding, and shield layout until radiated and conducted noise falls below limits in the relevant bands for residential and commercial settings. This reduces the chance of failing formal EMC tests, which would delay product launch and increase expense due to redesign and retesting.
Cooling system compliance testing
For high-power blenders that run near 2 kW or more, they test the cooling passage around the motor, bearings, and electronics. They log temperature rise at various load cycles, jar fill levels, and duty cycles which correspond to how cafés or hotel kitchens use them. They test that contact surfaces remain within safety limits and that internal components are rated beneath those of plastics, varnish, and grease. This information backs up safety files for regulators and demonstrates the unit will not overheat during heavy tasks like thick mixes, ice crush cycles, or extended batch blending.
Traceability documentation
OEMs create traceability from raw material to unit. Every lot of Tritan, stainless steel, gasket rubber and lubricant connects to supplier certificates displaying REACH, FDA, EU 1935/2004, 3-A, NSF 538 and ISO 21469 status where applicable. They label batches with barcodes or QR codes. More sophisticated facilities incorporate IoT sensors or blockchain-based ledgers so they know exactly when, where and how each was constructed. This assists with recalls, audits and quick root-cause investigations if a field issue arises in one market or region.
Certification maintenance
Post-launch, OEMs consider certification a living process. Professional OEM manufacturers monitor regulatory updates across target markets. If they switch a supplier, resin grade, lubricant, or even jar geometry, they risk review, re-run key tests, and update files. They conduct regular sample testing from production to verify that day-to-day builds still comply with EMC, hygiene, and material standards, so labels on the bottom of the blender remain accurate for years.
How to Avoid Certification Fraud in the Blender Industry

Purchasers should verify every certificate and not rely on a logo.
Reused test reports
Importers should request test reports that correspond to the exact blender model, wattage, and rated voltage. If the same report shows up for dozens of models with different motors or jars, it is probably recycled. Certification numbers and report dates should be cross-checked against official databases.
Edited PDFs
Importers ought to scan PDF certificates for funky fonts, fuzzy logos or copy-paste seams. They can match the file to samples on the certifier’s site and verify the certificate ID or NSF/ANSI Standard 8 listing in the database.
Invalid lab references
Importers can verify if the test lab appears on an accreditation body site and if its scope includes Low Voltage, EMC, or Machinery tests for food equipment. Missing accreditation numbers or vague addresses are red flags. Any CE or UKCA claim that refers back to such labs requires further evidence.
Mismatched model numbers
Importers have to match the model number on the nameplate, packaging, test reports, and Declaration of Conformity. Small tweaks, like additional letters, can obscure non-compliant production runs. Any discrepancy between documentation and product labeling must be formally clarified by the manufacturer before importation.
Final Thoughts: Choosing a Certification-Ready Commercial Blender Supplier
Commercial blender certifications are not simply labels on a nameplate. They represent a structured compliance system that protects importers, distributors, and end users from legal, safety, and financial risk.
Before selecting a supplier, verify that commercial blender certifications align with your target market requirements and that documentation is transparent, traceable, and current.
A certification-ready OEM partner reduces delays, avoids re-testing costs, and supports long-term distributor growth.
Looking for a structured way to explore ElectMix insights? Visit the ElectMix Knowledge Center to browse all categories, featured articles, and B2B resources in one place.
Frequently Asked Questions
What commercial blender certifications are required in the EU?
In the European Union, commercial blender certifications primarily include CE marking under the Low Voltage Directive (2014/35/EU) and the Electromagnetic Compatibility Directive (2014/30/EU). Most high-power commercial blenders are tested according to EN 60335-1 and EN 60335-2-14 for electrical and mechanical safety.
In addition to CE compliance, distributors must ensure conformity with RoHS Directive 2011/65/EU for restricted hazardous substances and REACH Regulation (EC) No 1907/2006 for chemical safety. For food-contact components such as jars, gaskets, and blades, compliance with Regulation (EC) No 1935/2004 and Regulation (EU) No 10/2011 is required.
Without proper commercial blender certifications in the EU, products may face customs rejection, market surveillance penalties, or legal liability for importers.
Is UL certification mandatory for commercial blenders in the U.S.?
UL certification is not federally mandated by law in the United States; however, it is effectively required in most commercial environments. A UL certified commercial blender is typically evaluated under UL 982 or related safety standards for motor-operated food preparation equipment.
Most commercial kitchens, restaurant chains, hospitals, and institutional buyers require UL listed appliances to pass local electrical inspections and insurance reviews. In many jurisdictions, building and fire codes reference nationally recognized testing laboratories (NRTLs), making UL certification practically essential for commercial blender compliance.
Without UL certification, distributors may encounter inspection failures, installation restrictions, or insurance coverage challenges.
Why is NSF important for commercial blender hygiene compliance?
NSF certification, commonly evaluated under NSF/ANSI 8, focuses on sanitary design, cleanability, and material safety in commercial food preparation equipment. Unlike general electrical safety certifications, NSF addresses how easily a commercial blender can be cleaned and whether food-contact surfaces meet hygiene standards.
NSF commercial blender certification verifies that:
- Food-contact materials are safe and compliant
- Surfaces are smooth and free of contamination traps
- Components withstand repeated sanitation cycles
- The design minimizes bacterial growth risks
For foodservice chains, hospitality groups, and regulated kitchens, NSF certification is often a purchasing requirement. It enhances credibility during health inspections and supports long-term compliance in high-volume environments.
How can distributors verify commercial blender certifications?
Distributors should implement a structured verification process when reviewing commercial blender certifications.
Best practices include:
- Requesting complete test reports rather than summary certificates
- Verifying report numbers and laboratory accreditation (ISO/IEC 17025)
- Confirming that the tested model matches the production model
- Checking certificate validity dates and surveillance status
- Cross-referencing certification numbers with official databases (UL, NSF, EU Declaration of Conformity)
- Reviewing factory audit documentation to confirm ongoing compliance
Certification verification reduces the risk of fraudulent documents, outdated reports, or mismatched model approvals. A reliable supplier should provide transparent documentation and maintain an organized compliance file for each commercial blender platform.
Marketing & Product Lead at ElectMix | Innovating Commercial Blenders & Home Appliances | Driving Growth & Development