Skip to content
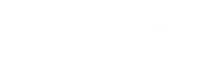

Juice yield tells you how much usable juice you obtain from a known quantity of fruit or vegetables. For a juice bar, café, bottled-juice business, distributor, or private-label buyer, it is more than a technical specification. It affects ingredient cost, servings per batch, waste volume, production planning, and the real payback of a juicer.
A basic weight-based formula is:
Juice yield (%) = mass of collected juice ÷ mass of prepared produce fed into the juicer × 100
However, commercial buyers should also track saleable yield: the volume of juice that can actually be served or bottled after foam, sediment, transfer loss, and recipe requirements are considered.
A higher number can improve profitability, but only when the test uses the same produce, preparation, machine settings, collection method, and operating conditions. Supplier claims measured under different conditions should not be compared as if they were equivalent.
What Does Juice Yield Mean?
Juice yield is the relationship between the raw produce entering a juicing process and the juice collected from it.
If you feed 1,000 grams of prepared apples into a juicer and collect 700 grams of juice, the measured juice yield is:
700 g ÷ 1,000 g × 100 = 70%

The remaining mass may include pulp, peel, seeds, retained liquid inside the machine, foam, residue on components, and unrecorded process loss.
That sounds straightforward, but the term is often used loosely in marketing. One supplier may calculate yield from whole produce before trimming. Another may weigh the edible prepared portion. A third may report juice volume in millilitres against produce mass in grams. Some may include foam or suspended pulp; others may filter the juice before measuring it.
Unless the test method is stated, “high juice yield” is not a complete or directly comparable performance claim.
Juice Yield, Extraction Efficiency, and Throughput Are Not the Same
Commercial buyers often see these terms grouped together, but they describe different parts of machine performance.
| Metric | What it measures | Why it matters |
| Juice yield | Collected juice compared with produce input | Ingredient utilization and potential servings |
| Saleable yield | Juice that can actually be served or bottled | Revenue-generating output |
| Extraction efficiency | How much of the produce’s available juice is recovered | Technical extraction performance |
| Throughput | Produce processed per unit of time | Service speed and labor planning |
| Pulp dryness | Moisture remaining in discharged pulp | Useful observation, but not a complete yield measurement |
| Process loss | Material not accounted for as juice or discharged residue | Transfer, leakage, retention and measurement control |
A machine can have good extraction yield but low throughput. Another can process produce quickly but leave visibly wet pulp. A third can collect a high volume that contains excessive foam or suspended solids and therefore produces less saleable juice after settling or filtering.
This is why a business should not evaluate a juicer using one number alone.
If you are still deciding which machine type and workflow fit your operation, begin with ElectMix’s complete guide to choosing a cold press juicer for business use.
Two Yield Measures Commercial Buyers Should Track

1. Weight-Based Extraction Yield
This is the most controlled method for comparing machines.
Juice Yield (%)=Mass of Collected JuiceMass of Prepared Produce Input×100\text{Juice Yield (\%)}= \frac{\text{Mass of Collected Juice}}{\text{Mass of Prepared Produce Input}} \times 100Juice Yield (%)=Mass of Prepared Produce InputMass of Collected Juice×100
Weight is normally more reliable than volume for comparison because juice density, pulp content and foam can change the relationship between grams and millilitres.
Use a calibrated scale and tare the collection container before each test.
2. Saleable Juice per Kilogram of Produce
For day-to-day business decisions, this measure is often more useful:
Saleable Yield=Final Usable Juice VolumeProduce Input in kg\text{Saleable Yield}= \frac{\text{Final Usable Juice Volume}}{\text{Produce Input in kg}}Saleable Yield=Produce Input in kgFinal Usable Juice Volume
For example:
- Prepared produce input: 5 kg
- Juice collected immediately: 3.6 L
- Foam, filtering and transfer loss: 0.2 L
- Saleable juice: 3.4 L
The operational result is:
3.4 L ÷ 5 kg = 0.68 L of saleable juice per kg of produce
If each menu serving is 340 mL, that batch provides:
3.4 L ÷ 0.34 L = 10 saleable servings
This number connects machine performance directly to recipe costing and inventory planning.
Why Pulp Dryness Is Only a Clue
Dryer pulp usually suggests that more liquid has been separated, but it is not enough to establish a yield percentage.
Pulp may look dry because:
- the produce itself contained less moisture;
- the screen allowed more fine solids into the juice;
- the pulp was compressed differently;
- the batch was fed more slowly;
- the produce was stored longer;
- part of the liquid remained inside the juicer;
- the output was collected with more foam.
Use pulp condition as a practical observation, not as a substitute for weighing the input and output.
A useful test record can include:
- juice mass;
- saleable juice volume;
- pulp mass;
- visual pulp moisture;
- foam volume;
- residue retained in the machine;
- test duration;
- preparation time;
- cleaning time.
Together, these results explain far more than a photograph of pulp.
A Repeatable Commercial Juice-Yield Test
To compare juicers fairly, use a controlled procedure.
Step 1: Define the Business Use Case
Choose ingredients that represent the actual menu or target market.
A juice bar selling leafy-green blends should not select a machine based only on an apple test. A hotel breakfast operation may care more about orange, apple, pineapple and carrot. A distributor serving home users may require a broader mix and simpler preparation.
Create at least three test groups:
- Firm produce: apples or carrots
- Soft or fibrous produce: pineapple, cucumber or celery
- Leafy or mixed recipe: spinach, kale, celery and apple, where relevant
Do not assume the same juicer will perform identically across all categories.
Step 2: Standardize the Produce
Record:
- variety;
- supplier or batch;
- ripeness;
- storage time and temperature;
- washed weight;
- trimming method;
- prepared input weight;
- piece size;
- whether peel, core or seeds were removed.
Produce condition can materially change the result. Research on mechanical juice extraction has likewise shown that factors such as maturity, processing conditions and extraction method influence yield; the result cannot be attributed only to the machine.
Step 3: Prepare the Machine
Before each comparison:
- assemble the correct auger and screen;
- confirm all seals are installed;
- ensure the filter is clean;
- use the same operating mode;
- allow the machine to reach the same starting condition;
- position and tare the collection containers;
- follow the manufacturer’s continuous-use limits;
- confirm that no juice remains from a previous batch.
If one machine uses a fine screen and another uses a coarse screen, record that difference. Screen selection may change both the measured yield and the texture of the output.
Step 4: Control the Feeding Method
Use the same:
- input weight;
- piece size;
- feed sequence;
- feed rate;
- operator;
- pusher technique;
- total test time definition.
Do not force produce into one machine while slowly feeding another. Excessive pressure can affect extraction, blockage, pulp consistency and motor load.
Step 5: Collect and Measure
At the end of the agreed processing period:
- Allow a fixed drainage time, such as 30 or 60 seconds.
- Weigh the collected juice.
- Weigh the discharged pulp.
- Record visible residue retained in the chamber.
- Measure foam and separation after a defined settling time.
- If filtering is part of normal service, filter every sample using the same method.
- Measure the final saleable volume.
- Record processing and cleaning time.
Do not quietly pour trapped liquid from one machine into the collection container unless the same recovery method is used for all machines and reflects normal operation.
Step 6: Repeat the Test
One batch can be distorted by produce variation or operator behavior.
Run at least several repeat trials for internal comparison and calculate the average. Also review the range between results. A machine that produces 72%, 61%, and 70% is less predictable than one that produces 68%, 69%, and 68%, even though their averages may appear similar.
For supplier qualification or marketing claims, the sampling plan and required number of runs should be agreed with the relevant technical team or laboratory.

Worked Example: Turning Yield Into Cost per Serving
Consider two candidate juicers processing the same prepared apple batch.
| Item | Juicer A | Juicer B |
| Prepared apple input | 10 kg | 10 kg |
| Ingredient cost | $20.00 | $20.00 |
| Juice collected | 7.2 kg | 6.7 kg |
| Measured weight yield | 72% | 67% |
| Final saleable juice | 6.8 L | 6.4 L |
| 340 mL servings | 20 | 18 full servings |
| Produce cost per full serving | $1.00 | $1.11 |
Based only on produce use, Juicer A saves approximately $0.11 per full serving in this test.
If the business sells 100 comparable servings per day over 300 operating days, the theoretical ingredient difference would be:
$0.11 × 100 × 300 = $3,300 per year
This is an illustrative calculation, not a universal saving. Actual results depend on local produce prices, recipes, trimming loss, seasonal variation, serving size, machine consistency and waste handling.
It also does not yet include labor.
If Juicer A requires substantially more cutting, slower feeding or longer cleaning, some ingredient savings may be offset by staff cost. A proper purchase decision should therefore compare:
Total Cost per Saleable Serving=Produce Cost + Labor + Consumables + Expected Operating CostNumber of Saleable Servings\text{Total Cost per Saleable Serving} = \frac{ \text{Produce Cost + Labor + Consumables + Expected Operating Cost} }{ \text{Number of Saleable Servings} }Total Cost per Saleable Serving=Number of Saleable ServingsProduce Cost + Labor + Consumables + Expected Operating Cost
Juice yield is important because it changes the denominator—but it is not the entire business model.

Why Juice Yield Matters to Commercial Buyers
Lower Ingredient Cost
Produce is a recurring expense. Even a modest difference in usable output can become meaningful when repeated across many servings, stores or operating days.
The benefit is usually strongest when:
- ingredients are expensive;
- recipes use leafy greens or specialty produce;
- daily volume is high;
- produce prices fluctuate;
- the business operates across multiple locations;
- bottled recipes require fixed fill volumes.
More Predictable Menu Costing
If yield changes widely between batches, the purchasing team cannot reliably forecast:
- kilograms required per day;
- servings per case of produce;
- gross margin by recipe;
- production time;
- inventory safety stock;
- daily waste volume.
Consistency can be commercially more valuable than one exceptional yield result.
Less Organic Waste
Higher recovery can reduce the mass of wet pulp requiring handling. This may lower bin volume, leakage and disposal frequency.
However, “less waste” should not be claimed solely from juice yield. Businesses may reuse pulp in food products, composting or other processes, and the practical value depends on local operations. Energy, water, packaging and cleaning requirements also belong in a broader sustainability assessment.
Better Production Planning
Yield helps a bottled-juice operation estimate how much produce is required for a planned filling run.
If 500 bottles require 250 L of saleable juice and the validated recipe produces 0.62 L per kilogram, theoretical prepared produce demand is:
250 L ÷ 0.62 L/kg = approximately 403 kg
A purchasing team would then add an appropriate allowance for normal process variation, quality sorting and operational loss.
Stronger Equipment Sales Conversations
For distributors and OEM buyers, verified yield data can make a product presentation more useful. Instead of saying “extracts more juice,” you can explain:
- which ingredients were tested;
- how produce was prepared;
- input and output values;
- screen and operating mode;
- average of repeated runs;
- saleable volume;
- comparison limitations.
That is more credible than an isolated percentage with no method.

Why the Highest Yield Is Not Automatically the Best Result
A juicer should not be optimized for one output number while ignoring the product customers actually want to sell.
Juice Texture and Pulp Level
A coarse screen may allow more fine solids into the collection container. This can increase collected mass but may produce a texture that does not suit the recipe or customer.
If a business filters the juice afterward, the final saleable yield may be lower than the initial measurement.
Foam and Separation
Foam can make immediate volume readings misleading. A container may look fuller without containing proportionally more saleable liquid.
Use mass measurements and a defined settling period. For bottled products, evaluate the juice under the business’s actual filling and holding conditions.
Throughput and Queue Time
A machine that produces slightly more juice but processes too slowly may not fit a high-demand counter.
Commercial evaluation should measure:
- kilograms processed per hour;
- active operator time;
- waiting and drainage time;
- interruptions for blockage;
- cleaning frequency;
- servings completed during peak service.
Cleaning and Changeover
Yield may fall during service if pulp builds up on the screen. Stopping to clean can restore performance but interrupts production.
The detailed relationship among cleaning, maintenance, labor and downtime will be covered in Article 15, Cold Press Juicer Maintenance: How to Reduce Downtime and Costs.
Product Quality and Recipe Requirements
Yield does not by itself establish nutrient retention, flavor, shelf life or safety. These require appropriate testing and handling controls.
Extraction method can influence properties such as soluble solids, color, turbidity and acidity. A published study comparing mechanical extraction methods for apple juice, for example, evaluated several quality indicators rather than treating output quantity as the only measure. See the open-access study on mechanical juice extraction methods.
What Changes Juice Yield?
Produce Type
Water-rich cucumber behaves differently from fibrous celery, leafy greens or dense carrots. A percentage obtained with watermelon or pineapple should not be presented as the machine’s universal yield.
Variety, Ripeness and Storage
Two batches of the same fruit can contain different amounts of water and structural fiber. Ripeness and storage conditions may affect softness, moisture and separation behavior.
Compare machines using produce from the same batch whenever possible.
Trimming and Preparation
Peeling, coring and removing damaged material changes the input basis. Report whether yield is calculated from whole purchased produce or prepared edible produce.
Both figures can be useful:
- Purchase-to-saleable yield helps business costing.
- Prepared-feed extraction yield helps machine comparison.
Do not mix them.
Cutting Size and Feed Rate
Pieces that are too large may not feed consistently. Pieces that are unnecessarily small increase labor. Feeding too quickly can overload the chamber; feeding too slowly may improve extraction but reduce practical output.
The right test balances machine performance with realistic staff behavior.
Auger and Chamber Design
Auger geometry, compression path, chamber clearance and outlet resistance influence how produce is crushed and conveyed.
These design elements should be evaluated as a system. A more aggressive compression setting is not automatically better if it increases blockage, component stress or unwanted solids.
Screen Design
Hole size, open area, material, stiffness and cleaning condition influence separation.
A screen can affect:
- pulp level;
- flow rate;
- pressure;
- clogging;
- final texture;
- cleaning time;
- measured collected mass.
Seals and Assembly
Incorrectly installed silicone parts or worn seals can cause leakage, internal bypass or inconsistent pressure. Distributor testing should use the final production parts and the assembly instructions intended for customers.
Operator Technique
Different operators may apply different pressure, feeding rhythm and preparation methods. A good commercial machine should not depend on one unusually skilled tester to achieve its claimed performance.
Machine Condition
A clean new screen may perform differently from a partially blocked or worn one. Yield evaluation should include repeated operation, not only a showroom demonstration.
How to Compare Supplier Yield Claims Fairly
When a supplier presents a yield percentage, ask for the complete test context.
| Question | Why it matters |
| What ingredient and variety were used? | Yield varies by produce |
| Was input measured before or after trimming? | Changes the calculation base |
| Was juice measured by mass or volume? | Foam and density affect volume |
| Was pulp filtered from the juice? | Fine solids can increase collected mass |
| Which screen and mode were used? | Changes texture and separation |
| What was the feed rate? | Can trade throughput for extraction |
| How long was drainage allowed? | Affects collected output |
| How many trials were run? | One result may not be representative |
| Was the percentage an average or best run? | Best-case figures can mislead |
| Was the tested unit the production model? | Prototype performance may not transfer |
| What was the saleable yield? | Connects test output to revenue |
| What cleaning was required between batches? | Affects real workflow |
If the method is unavailable, treat the number as a lead for further testing—not as a guaranteed commercial result.
Do not compare a supplier’s “up to” claim against another supplier’s average field result.
A Distributor and OEM Buyer Test Plan
A distributor needs more than a high number. The product must be repeatable, explainable and suitable for the intended customer.
Before approving a model, test:
- At least three relevant ingredient groups
- Repeated batches from the same produce lot
- Weight-based yield and saleable volume
- Output consistency between runs
- Throughput and active labor time
- Pulp condition and machine retention
- Foam and texture after settling
- Assembly and operator variation
- Performance before and after repeated use
- Cleaning and reassembly
- Final production components and screen
- Available spare and wear parts
For broader model selection—covering workflow, downtime, materials, spare parts and target channel—refer to How to Choose a Cold Press Juicer for Business Use.
Buyers comparing processing methods may also review Cold Press Juicer vs High-Speed Blender and ElectMix’s WT-J001 slow juicer product page.
A Practical Yield Evaluation Sheet
Use the following fields for every trial:
| Test field | Result |
| Machine model and revision | |
| Auger and screen | |
| Produce and variety | |
| Purchase weight | |
| Prepared input weight | |
| Preparation method | |
| Starting temperature | |
| Feed size and rate | |
| Juice mass | |
| Initial juice volume | |
| Saleable juice volume | |
| Pulp mass | |
| Foam or filtering loss | |
| Material retained in machine | |
| Processing time | |
| Active operator time | |
| Cleaning time | |
| Repeated-run average | |
| Observed blockage or leakage | |
| Taste and texture notes |
This turns yield from a marketing phrase into a controlled commercial measurement.
How ElectMix Approaches Juice-Yield Evaluation
ElectMix develops and supplies juicing and blending equipment for distributors, private-label brands and commercial buyers.
For an OEM or bulk-supply project, useful evaluation starts with the buyer’s real ingredients, service model and target market. Depending on the project stage, our team can help clarify:
- intended ingredients and recipes;
- required output and daily volume;
- auger and screen configuration;
- sample-testing conditions;
- juice, pulp and throughput measurements;
- cleaning and reassembly workflow;
- food-contact component information;
- accessory and spare-part requirements;
- product labeling and packaging;
- production-version confirmation.
Yield results should be attached to a stated method and sample configuration. ElectMix does not recommend choosing a juicer from an isolated headline percentage alone.
If you are evaluating a slow juicer for distribution, foodservice use or private labeling, send us your expected ingredients, daily volume, serving format and target market. We can use those details to discuss a more relevant sample test.
Frequently Asked Questions
What is a good juice yield for a commercial juicer?
There is no universal percentage that applies to every ingredient and machine. Produce type, ripeness, trimming, screen, feed rate and measurement method all change the result. A good commercial result is one that is repeatable for the business’s actual recipes and produces an acceptable cost per saleable serving.
How do you calculate juice yield?
For a controlled weight-based test, divide the mass of collected juice by the mass of prepared produce fed into the juicer, then multiply by 100. Record the method, produce condition, screen, feed rate and drainage time.
Should juice yield be measured by weight or volume?
Weight is generally better for controlled machine comparison because foam, density and suspended solids can distort volume readings. Businesses should also measure final saleable volume because that determines servings or bottle output.
Does dry pulp always mean higher juice yield?
No. Dry pulp is a useful observation, but it does not account for juice trapped inside the machine, fine solids entering the juice, produce moisture or process loss. Input and output should be weighed.
Can a slower juicer produce more profit than a faster one?
It can, if higher saleable yield reduces ingredient cost enough to offset slower processing and labor. The opposite can also be true during peak service. Compare total cost per saleable serving and servings per hour.
Why do two tests of the same juicer give different yields?
Differences may come from produce variety, ripeness, temperature, piece size, feed rate, screen cleanliness, assembly, drainage time and operator technique. Use the same produce lot and repeat the test.
What should distributors request from a juicer supplier?
Request the test method, ingredient, preparation basis, input and output measurements, number of trials, average result, screen and mode, production-model confirmation, throughput, cleaning conditions and sample availability for independent verification.
Conclusion
Juice yield matters because produce that remains in wet pulp, foam, machine residue or process loss cannot be sold as a full serving.
But the most useful commercial question is not:
“Which machine has the highest advertised percentage?”
It is:
“Which machine gives us the most consistent saleable output at an acceptable total cost, speed, texture and cleaning workload for our actual menu?”
Measure yield by weight. Track saleable volume. Standardize the produce and operating method. Repeat the test. Then connect the result to ingredient cost, labor and servings.
That is how commercial buyers turn juice yield into a purchasing decision rather than a marketing claim.
Marketing & Product Lead at ElectMix | Innovating Commercial Blenders & Home Appliances | Driving Growth & Development